Choosing the best Inverter Igbt Welder requires more than comparing price tags and advertised amperage. A practical buyer examines arc stability, duty cycle, input power, portability, protection systems, and local service support. These details matter when a machine runs beside a dusty workshop bench or powers a long weld on thick steel.
Welding educator Jody Collier offers a useful reminder: “The best welder is the one that matches the job and the person using it.” That principle keeps the decision realistic. A compact Inverter Igbt Welder may suit home repairs, farm maintenance, and light fabrication. A professional shop may need higher duty cycles, dependable thermal protection, and consistent performance during repeated passes. More power is not always better.
The strongest models use IGBT technology to control current efficiently and maintain a steadier arc. Look for clear specifications, honest duty-cycle ratings, overheat protection, and accessible replacement parts. Check whether the stated output applies at your local voltage. That point is easy to miss.
Hands-on testing still matters. A machine that starts smoothly, produces less spatter, and responds quickly to small current changes can save electrodes, time, and frustration. Yet no inverter is perfect. Some displays feel unclear. Some cooling fans sound harsh. Reviews may also exaggerate performance.
This guide compares leading options through measurable features and real workshop needs. It also questions attractive claims, because reliability is proven during ordinary work, not only in product photographs.
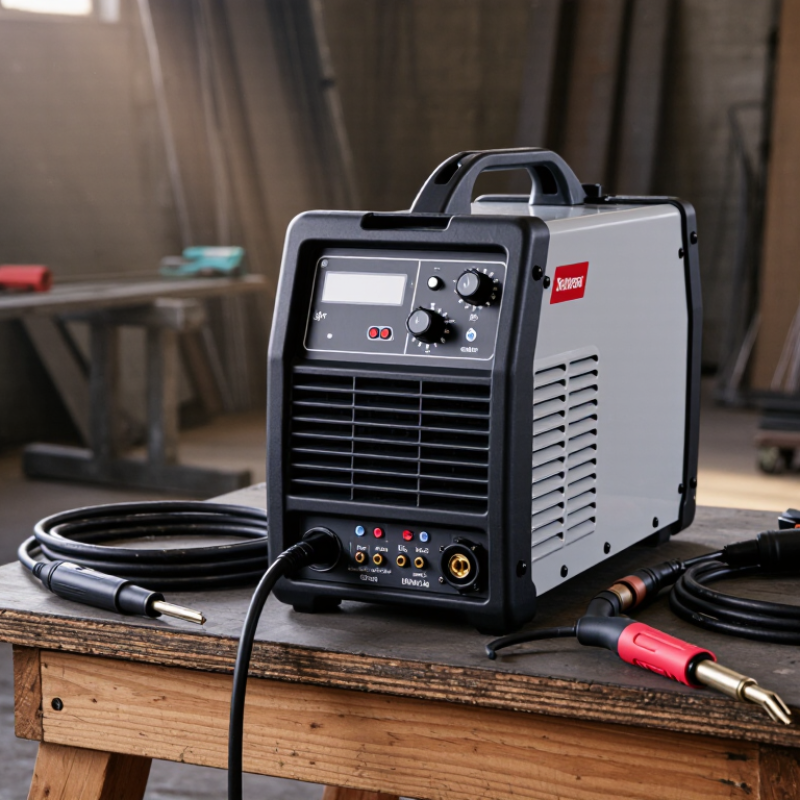
An inverter IGBT welder uses insulated-gate bipolar transistors to switch electrical power at high frequency. In simple terms, it converts incoming power into controlled welding current through several electronic stages. The high-frequency design allows a smaller transformer than many traditional welders use. That often means a lighter machine that is easier to carry between a bench and a job site.
What does that feel like in use? The machine may start an arc smoothly and maintain steadier current as you move along a joint. On a steel coupon, you can hear the arc’s crackle change when the gap grows too wide. Inverter controls help adjust output, but they cannot replace sound technique. Not magic. IGBT technology describes the power electronics, not every feature or the quality of the finished weld. Check the rated output, input supply, duty cycle, and compatible welding processes before buying. A compact unit may handle short repairs well, yet need cooling breaks during longer runs. I once assumed a lighter welder meant less compromise; that is not always true, but the rating plate deserves a closer look.
An IGBT inverter welder first converts incoming AC power into DC. Its insulated-gate bipolar transistors then switch that current rapidly, creating high-frequency power. A transformer changes the voltage, and the output is converted and regulated for welding. The control circuit adjusts current to suit the selected setting. That is the core idea.
This compact process can make the machine lighter and help maintain a steadier arc. For example, a controlled output can make it easier to keep a short arc while welding a steel bracket. But inverter technology alone does not guarantee good welds. Cable connections, input voltage, cooling, and operator technique still matter. Heat still matters. A machine’s duty-cycle rating also deserves attention; a small unit may need cooling breaks during longer jobs.
Tips: Match the welder’s output range to your usual material thickness and electrode size. Check its duty cycle at the amperage you expect to use, not just its maximum rating. Keep vents clear, use sound cables, and follow the manual’s electrical and protective-equipment guidance. One detail is easy to overlook: advertised maximum amperage says little about how consistently a welder performs during a full work session.
| Topic or Process | How It Works / Typical Range | Advantages | Best Suited To | What to Check Before Buying |
|---|---|---|---|---|
| IGBT inverter technology | The input is rectified to DC, then insulated-gate bipolar transistors (IGBTs) switch it at high frequency. A compact transformer and output circuitry convert and regulate the power for welding. | High-frequency conversion can make the power source smaller and lighter than a traditional line-frequency transformer welder. Electronic control can help regulate the welding output. | Users who need a portable power source and adjustable output for suitable welding processes. | Check the rated output, input requirements, duty cycle, protections, and service support. IGBT technology alone does not determine weld quality or reliability. |
| MMA / Stick (SMAW) | Typical compact machines provide about 20–200 A, though the range varies. The arc melts a flux-coated consumable electrode; its flux helps shield the weld pool. | Relatively simple setup, no external shielding-gas cylinder, and suitable for many outdoor repair tasks. | General repairs, maintenance, and work where portability or outdoor use matters. | Confirm supported electrode sizes, input supply, usable output at the required current, and duty cycle. |
| DC TIG (GTAW) | Typical compact units may offer roughly 10–200 A. A non-consumable tungsten electrode creates the arc; shielding gas is supplied separately, and filler metal can be added as needed. | Precise heat control and clean welds when the operator and joint preparation are suitable. | Detailed work on steel and stainless steel, including thinner material when correctly set up. | Check whether a TIG torch, gas controls, and high-frequency or lift start are included. DC-only TIG is generally not the standard choice for welding aluminum. |
| AC/DC TIG | Provides DC output for many steels and AC output commonly used for aluminum TIG welding. Available current and features depend on the machine. | Supports a wider range of TIG materials and applications than a DC-only unit. | Fabrication or repair work that includes aluminum as well as steel or stainless steel. | Compare AC balance and frequency controls, maximum output, input power needs, and the accessories supplied. |
| MIG / MAG (GMAW) | Typical light-duty inverter units may offer about 30–250 A. A continuously fed wire electrode forms the arc; shielding gas is used for MIG/MAG, while some machines also support gas-shielded or self-shielded flux-cored wire. | Continuous wire feed can support faster welding on suitable jobs and reduce frequent electrode changes. | Workshop fabrication, sheet-metal work, and repeated welds with a compatible wire and setup. | Check wire diameter range, spool capacity, feed adjustment, gas compatibility, and the machine’s rated duty cycle. |
| Duty cycle and thermal rating | Duty cycle is the portion of a stated test interval that a welder can operate at a specified current before cooling is required. For example, 60% over a 10-minute interval means 6 minutes welding and 4 minutes cooling at the stated conditions. | A clear rating helps indicate whether the machine can sustain the intended workload. | All buyers, especially those planning long welds or high-current work. | Compare duty-cycle figures at the same current and test standard; higher current commonly means a lower duty cycle. |
| Input power and portability | Small welders may be designed for a single-phase supply, but voltage, input current, plug, and output capability vary by model. A higher welding output can require more input power. | A suitable supply and manageable weight make the machine practical at the intended work site. | Home workshops, mobile repair, and jobs where access to power is limited. | Verify the exact supply voltage, circuit capacity, extension-lead requirements, machine weight, and local electrical compatibility. |
| Practical buying choice | There is no single best IGBT inverter welder for every user. The right choice depends on process, materials, thickness, available power, workload, and operator experience. | Matching features to the actual job avoids paying for capabilities that are not needed or choosing a machine that is underpowered. | Choose MMA for versatile basic repair, TIG for controlled precision work, MIG/MAG for continuous wire-feed work, or AC/DC TIG when aluminum TIG capability is required. | Prioritize process compatibility, realistic rated output, duty cycle, input supply, included accessories, safety features, warranty, and accessible service. |
Current ranges are indicative examples for compact inverter welders, not universal specifications. Always check the machine’s nameplate and technical manual; actual capability depends on the model, input supply, consumables, and operating conditions.
When comparing IGBT welders, start with the jobs you actually do: thin sheet repair, farm maintenance, or repeated work on thicker steel. Check the machine’s process options, input voltage, and usable current range. A high peak-amp figure looks impressive, but it says little about how long the welder can sustain that output. Numbers need context.
Read the duty-cycle rating at the stated amperage. A 60% rating generally means six minutes of welding in a ten-minute period, followed by cooling time. Compare ratings at the same current, and look for thermal-overload protection. IEC 60974-1 sets requirements for arc-welding power sources, including performance and safety; a clear rating plate helps you check what the machine claims. Hot start, arc force, and anti-stick functions can make stick welding easier, especially when striking an arc on a cold or rusty workpiece. Still, adjustment quality matters more than a long feature list.
Also consider weight, cable length, spare-part availability, and whether the controls are usable with gloves. The American Welding Society’s 2023 workforce data projected that the United States would need 360,000 new welding professionals by 2027. That is not a machine-performance measure, but it highlights why straightforward setup and service support matter. A compact welder can be convenient on stairs; a short lead can still make it frustrating beside a workbench. I would check the manual before buying, though manuals are not always clear.
For thin automotive panels and home repairs, choose an IGBT welder with stable low-amp control and a clear display. A 120-volt input suits light work, but thicker steel may require 240 volts and higher output. For farm gates or structural repairs, compare rated amperage with duty cycle, not peak amperage alone. IEC 60974-1 defines welding power-source ratings and testing, helping buyers compare specifications on a consistent basis. Still, real performance depends on cables, input supply, and operator technique.
For mobile maintenance, a compact unit with dependable stick welding can be easier to carry across gravel or up a ladder. For a workshop, MIG capability and a higher duty cycle reduce pauses on repeated joints. The American Welding Society’s 2023 workforce outlook projected that the United States would need 360,000 welding professionals by 2027, reflecting demand across varied work settings. That figure does not identify a best machine; it underlines why matching equipment to the job matters. A confusing point: more features do not always mean cleaner welds.
Tips
Check the duty cycle at your intended amperage; IEC ratings use a 10-minute test period. For example, a 40% rating means about four minutes of welding, followed by cooling time. Test a sample joint before buying, if possible. Short beads can hide heat limits.
Before striking an arc, inspect the power lead, torch cable, plug, and return clamp for cuts or loose connections. Look closely. Dust can clog cooling vents and raise the inverter’s temperature, so clean them as the manual directs. Keep the unit dry, and never clean it while connected to power. Internal capacitors may retain a dangerous charge after shutdown; leave internal repairs to qualified technicians. A rushed check can miss a damaged clamp. That is easy to overlook.
Control fumes at the source with suitable local exhaust ventilation, especially when welding coated or manganese-containing materials. NIOSH’s Pocket Guide to Chemical Hazards lists a recommended time-weighted exposure limit of 1 mg/m³ for manganese, measured as Mn. It is a useful reference, not a substitute for assessing the actual fume and work area. For fire prevention, OSHA’s 29 CFR 1910.252 calls for keeping combustibles at least 35 feet away where practicable. It also requires a fire watch for at least 30 minutes after welding ends. Keep a suitable extinguisher nearby, and check the work area before leaving. The last glance is not busywork.
Northeast Battery, a Stored Energy Holdings, Inc. Company