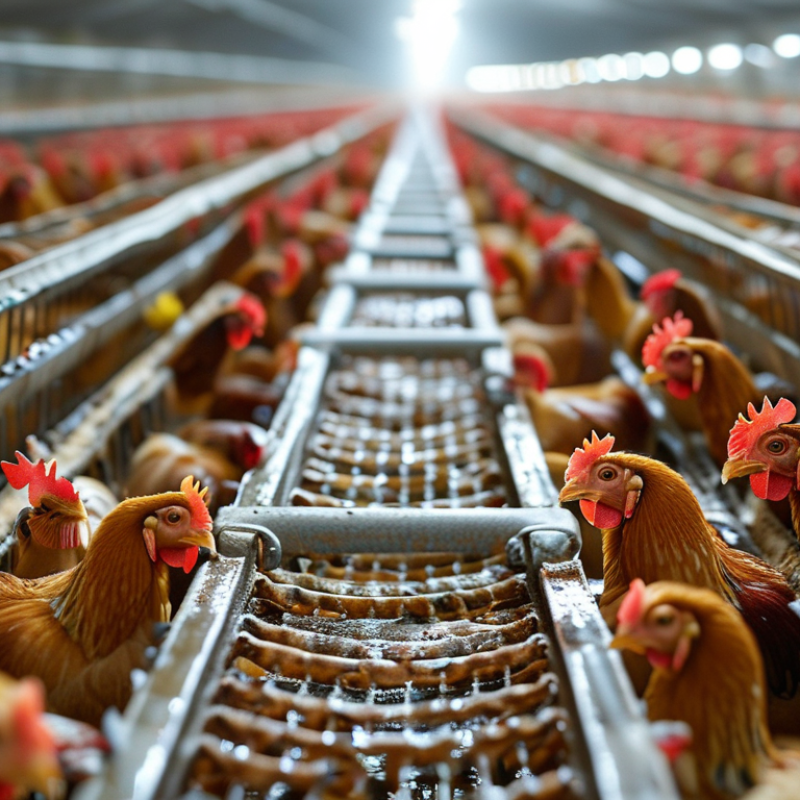
| Definition | Chicken cage manure belt | A continuous conveyor belt installed beneath or between poultry cage tiers to collect and transport chicken manure to a discharge point or manure processing area. |
| Primary function | Manure collection and removal | The belt reduces direct contact between manure and the poultry house floor, supports more frequent cleaning, and can help improve house hygiene when properly operated. |
| Common belt material | Polypropylene (PP) | PP is widely used because it is lightweight, moisture-resistant, relatively easy to clean, and suitable for repeated movement in poultry manure systems. |
| Typical belt width | Approximately 1,000–2,500 mm | The required width depends on the cage design, tier arrangement, manure volume, and conveyor frame. The belt should be wider than the effective manure-fall area to reduce spillage. |
| Typical belt thickness | Approximately 0.8–2.0 mm | Thicker belts generally provide greater resistance to tearing and deformation, while thinner belts may reduce system weight and initial material cost. The correct choice depends on span, tension, and manure load. |
| Surface design | Smooth or lightly textured surface | A smooth surface helps manure discharge and simplifies washing. Excessively deep textures may retain material and increase cleaning requirements. |
| Usable temperature range | Typically about −20°C to 60°C | The actual operating range depends on the belt formulation, storage conditions, cleaning method, and local climate. The supplier should confirm performance for the farm’s lowest and highest temperatures. |
| Drive arrangement | Motor-driven roller or sprocket system | The drive system pulls the belt through the cage row. Correct alignment, roller engagement, and tension are essential to prevent belt wandering, slipping, or edge damage. |
| Usual conveying speed | Approximately 5–20 m/min | The suitable speed depends on cage length, manure moisture, discharge capacity, and cleaning frequency. Excessive speed can increase spillage and mechanical stress. |
| Recommended belt qualities | Tear resistance, dimensional stability, and low water absorption | A suitable belt should resist cracking, stretching, edge fraying, and deformation during continuous operation. Material uniformity and reliable welded or mechanically joined seams are important. |
| Joint methods | Thermal welding, hot pressing, or mechanical fasteners | A welded joint can provide a smooth, low-profile connection when correctly made. Mechanical joints may simplify field installation but should be selected to avoid catching on rollers or cage components. |
| Cleaning requirements | Routine dry scraping and periodic washing | Removing excessive manure before it hardens helps reduce belt load. If water is used, the belt, frame, bearings, and electrical components should be compatible with the cleaning procedure. |
| Installation checks | Leveling, alignment, tension, and roller clearance | The conveyor frame should be straight and level. Insufficient or excessive tension can cause tracking problems, slipping, premature wear, or damage to the belt and drive components. |
| Important purchasing data | Length, width, thickness, joint type, and cage configuration | A buyer should provide the complete belt length, required width, thickness, number of tiers, cage-row layout, drive position, operating temperature, and expected cleaning method before requesting a quotation. |
| Supplier evaluation criteria | Material consistency, dimensional accuracy, sample testing, and after-sales support | Compare technical specifications rather than price alone. Check belt dimensions, seam quality, tensile performance, packaging, delivery capability, installation guidance, replacement-part availability, and warranty terms. |